The manufacturing landscape is undergoing a profound transformation, driven by the relentless pursuit of efficiency, quality, and adaptability. At the forefront of this revolution lies computer vision.
Indeed, manufacturers are actively prioritizing investments in the foundational technologies that underpin smart manufacturing. According to Deloitte’s 2025 Smart Manufacturing Survey, vision systems rank among the top investment priorities. In terms of respondents’ first and second priorities for the next 24 months, 28% reported vision systems.
This article will delve into core computer vision techniques, explore its diverse applications across the manufacturing lifecycle, and examine which one brings the highest ROI.
- Computer vision is one of the top investment priorities, with 28% of manufacturers planning to adopt vision systems by 2025 to boost efficiency and quality.
- CV enhances every production stage — from design validation and raw material inspection to real-time defect detection, packaging verification, and post-sale support.
- Operational efficiency and safety improve significantly through automated inspection, vision-guided robotics, inventory tracking, worker PPE monitoring, and hazard detection.
- Predictive maintenance is a high-ROI use case, with CV identifying wear, misalignment, and early equipment faults to prevent unplanned downtime.
- With the right software and an autonomous robot, Crunch-IS’s client achieved 98% face recognition accuracy and over 95% person detection precision, ensuring reliable identification in real-time.
What Is Computer Vision in Manufacturing?
Computer vision in manufacturing refers to the use of AI-powered cameras and algorithms that enable machines to “see”, interpret, and act on visual data. These systems automate inspection, assist robots, monitor production, improve safety, and support predictive maintenance.
In practice, computer vision systems for manufacturing transform raw visual input into structured insights that guide robotic arms, detect defects, verify labels, and track materials across the entire factory.
Benefits of Computer Vision in the Manufacturing Industry
Computer vision offers a wide array of significant benefits to the manufacturing industry, transforming traditional processes into smarter, more efficient, and safer operations. Here are some key advantages:
Enhanced quality control and defect detection:
- CV can inspect products with unparalleled speed and precision, detecting even subtle defects like cracks, scratches, misalignments, or color inconsistencies that might be missed by human inspectors.
- Unlike human inspectors who can suffer fatigue or subjectivity, computer vision provides consistent inspection standards, ensuring every product meets the same rigorous quality benchmarks.
- And by identifying defects early in the production line, manufacturers can reduce waste, rework costs, and prevent faulty products from reaching customers, protecting brand reputation and minimizing recall expenses.
Increased efficiency and productivity:
- Computer vision automates monotonous and time-consuming visual inspection tasks, freeing up human workers to focus on higher-value activities.
- Real-time visual data analysis helps identify bottlenecks, optimize assembly lines, and improve overall production throughput.
- Vision-guided robots can accurately pick, place, and assemble components, leading to greater precision, flexibility, and faster production cycles.
- CV can automatically track inventory levels, monitor material flow, identify misplaced items, and streamline warehouse operations.
Improved safety:
- Computer vision for manufacturing safety can continuously monitor compliance with regulations, detect if workers are wearing required Personal Protective Equipment (PPE) like helmets or gloves, and identify unsafe behaviors or conditions in real time.
- Systems can detect workers entering restricted zones, approaching dangerous machinery, or even signs of fatigue, triggering immediate alerts to prevent accidents.
- CV can assist in identifying emergencies like fires or leaks, enabling quicker response times.
Cost savings:
- Early defect detection significantly reduces the need for costly rework and minimizes material waste.
- Automation of inspection and other visual tasks can reduce reliance on manual labor.
- By monitoring equipment for signs of wear and tear, computer vision enables proactive maintenance, preventing unexpected breakdowns, costly repairs, and unplanned downtime.
Better decision-making:
- CV provides real-time data and analytics on production processes, quality, and safety, enabling manufacturers to make informed, data-driven decisions.
- Analyzing trends from visual data helps in continuous process improvement and optimization.
Computer Vision Use Cases in Manufacturing at All Production Stages
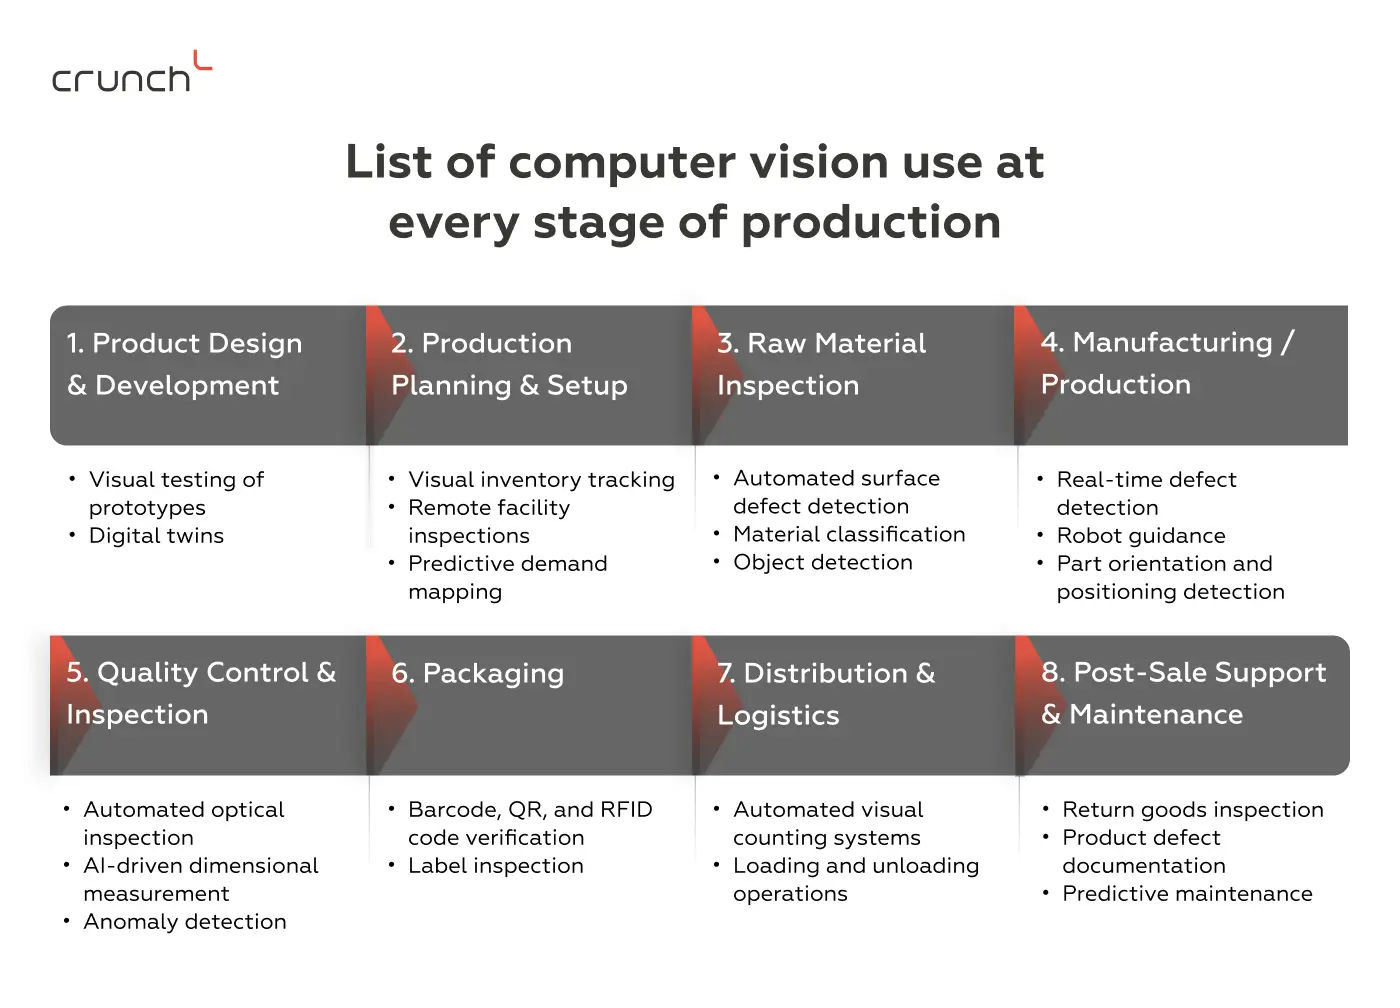
Manufacturing is rarely a straight line. It’s a cyclical, multi-phase process that involves design, testing, production, delivery, and often feedback and renewal. Computer vision can be implemented in every stage of manufacturing, if desired. We have compiled a comprehensive list outlining СV’s use at every stage of production:
1. Product Design & Development
The manufacturing lifecycle begins with concept and product design. At this stage, designers and engineers create sketches, 3D models, and technical drawings using CAD software. Materials are selected, costs are estimated, and sustainability is considered to ensure the product is both feasible and responsible.
With computer vision, however, teams can:
- accelerate design validation by visual testing of prototypes in simulated environments
- align virtual and physical versions in real-time using digital twins for more accurate testing
2. Production Planning & Setup
With a refined prototype in hand, companies move on to production planning and supply chain setup. This phase involves deciding how to produce the product on a larger scale.
Manufacturers source raw materials and components, set up partnerships with suppliers, and determine the most cost-effective and efficient production methods. They also establish logistics, train the workforce, and ensure that facilities and machinery are ready for operation. A clear production schedule and budget are created to guide the upcoming manufacturing process.
This stage can be enhanced by:
- visual inventory tracking using AI-enabled cameras to monitor raw material stock levels in real-time
- remote facility inspections with AI-assisted video feeds to verify machine placement, safety compliance, and workspace readiness
- predictive demand mapping powered by visual analytics of supply chain patterns, such as cargo movement, packaging density
3. Raw Material Inspection
Once materials and components have been sourced, manufacturers perform raw material inspections to ensure incoming supplies meet quality standards. This step helps prevent defective or non-compliant materials from entering the production line, which could lead to costly rework, delays, or product failures down the road.
Computer vision can improve this stage by:
- automated surface defect detection using high-resolution cameras to identify dents, rust, or scratches before materials enter production
- material classification to sort metals, plastics, or fabrics by type, grade, or color
- foreign object detection that flags contaminants like plastic or organic matter in raw supplies, especially in food or pharmaceutical manufacturing
4. Manufacturing / Production
In this phase, raw materials are transformed into finished goods through various manufacturing techniques such as machining, molding, or assembly line production. Modern manufacturing facilities often rely on automation, robotics, and digital monitoring systems to increase speed and precision.
Computer vision use cases in this phase include:
- real-time defect detection to identify cracks, misalignments, or deformities during machining, molding, or casting
- robot guidance powered by visual inputs, enabling precise assembly, welding, or gluing tasks with adaptive adjustments
- part orientation and positioning detection, allowing pick-and-place robots to identify and handle items correctly on the fly without manual intervention
5. Quality Control & Inspection
Once products are assembled, ensuring they meet quality standards is critical before packaging and distribution. This phase involves systematic inspections to verify dimensional accuracy, surface quality, functionality, and compliance with regulations.
Here’s how computer vision improves quality control in manufacturing:
- automated optical inspection (AOI) using high-resolution cameras and AI algorithms to detect micro-defects in PCBs, welds, or electronics
- AI-driven dimensional measurement, enabling non-contact precision checks of part size, shape, and alignment
- pattern and surface anomaly detection, identifying scratches, dents, or contamination in real time, with faster throughput than human inspectors
6. Packaging
After products pass quality control, they proceed to packaging, where they are prepared for safe delivery and sale. This step contains placing items into containers, applying labels, verifying codes, and ensuring packaging integrity. Errors at this stage can lead to regulatory issues, customer dissatisfaction, or supply chain delays.
Computer vision use cases in the packaging stage:
- high-speed barcode, QR, and RFID code verification, ensuring traceability and compliance before shipping
- computer vision-based label inspection to confirm correct placement, readability, and branding alignment
7. Distribution & Logistics
Once packaging is complete, products enter the distribution and logistics phase, where efficient handling and transportation are critical to maintaining product quality and timely delivery. This stage involves organizing shipments, tracking inventory, and managing the movement of goods through warehouses and transportation networks.
Computer vision applications in manufacturing’s distribution and logistics:
- automated visual counting systems use CV to quickly and accurately tally pallets and individual packages
- AI-powered cameras guide workers and robotic systems during loading and unloading operations, ensuring correct placement, optimizing space utilization, and preventing mishandling that could cause damage
8. Post-Sale Support & Maintenance
Even after the product reaches the customer, computer vision continues to play a role in ensuring satisfaction and operational efficiency. In post-sale support and maintenance, visual technologies help streamline returns, improve service quality, and extend the lifespan of equipment.
Computer vision solution for post-sale support and maintenance in manufacturing:
- return goods inspection using AI vision models to analyze items for signs of damage, tampering, or usage
- product defect documentation via customer-shared photos, which are then analyzed using machine learning models to identify issues, classify defects, and speed up the claims process
- predictive maintenance through visual monitoring of in-use equipment that allows businesses to detect early signs of malfunction and schedule proactive maintenance before breakdowns occur
Computer vision techniques in manufacturing
At its core, a CV system interprets visual data from a scene, translating it into a symbolic description that guides robotic operations and various industrial processes. To dive deeper into the fundamentals, explore our previous article: How Does Computer Vision Work? 6 Real-World Computer Vision Use Cases by Industry. This complex process involves several key techniques, including detection, recognition, segmentation, and 3D reconstruction.
1. Feature Detection
Computer vision relies on feature detection to identify crucial elements in images. This involves pinpointing key points (distinct regions like corners or specific shapes) and edges (boundaries between objects):
- key point detection can be either local search (ideal for continuous video streams) or global search (better for scenes with significant movement).
- edge detection identifies sudden changes in color or intensity. Methods range from gradient-based techniques and zero-crossing methods to advanced deep learning approaches using CNNs.
2. Recognition
Recognition allows computer vision to identify and classify objects or actions within an image or video. This capability is paramount for tasks like automated inspection, assembly verification, and worker safety monitoring. Recognition problems are generally grouped into four categories:
- instance recognition focuses on identifying a specific known object
- class recognition aims to identify any instance of a general category
- general category recognition is more complex, requiring both localization and classification of all objects in an image
- action recognition is a challenging and evolving area, focusing on understanding behaviors in videos, crucial for worker safety and autonomous systems in manufacturing
3. Segmentation
Segmentation involves labeling each pixel in an image according to the object it belongs to, providing a detailed understanding of object boundaries. This is essential for precise robotic manipulation.
Early segmentation techniques relied on region division and merging. More advanced algorithms employ consistency indicators like intraregional consistency and interregional dissimilarity.
Current trends in segmentation are moving towards 3D and 4D segmentation (3D segmentation targets three-dimensional images, while 4D segmentation incorporates the time dimension, enabling the analysis of dynamic scenes).
4. 3D Modeling
3D modeling in CV creates three-dimensional representations of objects or scenes, crucial for robot navigation and virtual prototyping. This field is broadly divided into two problems:
- Stereo correspondence builds 3D models from multiple 2D images by matching pixels across views.
- 3D reconstruction creates a 3D model from just one image. This started with “shape from shading” and evolved into “shape from X” methods like shape from texture and shape from focus. Recent deep learning algorithms have significantly advanced 3D reconstruction capabilities.
These CV techniques are continuously evolving, offering increasingly sophisticated solutions for smart manufacturing.
Crunch-IS Case Study: Securing Premises with AI-Powered Robotics (CV Technology)
In our recent collaboration with an AI startup in France we developed a powerful computer vision for their autonomous security robot. The client aimed to enhance security against intrusions at business premises.
The primary goal was to create software for autonomous robots that could accurately identify and process human presence and facial features.
Our Solution
Leveraging deep learning, our team developed high-performance computer vision software for the robot, enabling real-time detection and recognition. Our approach focused on three key areas:
- Face and eye detection. We built and normalized a diverse image dataset to ensure consistent and accurate face recognition across various conditions. This involved advanced feature extraction and identification.
- Person detection. Similarly, we collected and processed images to isolate human figures, training the system to account for diverse sizes and features for robust detection.
- Gate detection. To ensure seamless navigation, we integrated functionality for detecting and classifying objects like gates, giving the robot crucial spatial awareness for effective patrolling.
The implemented computer vision software delivered 98% face recognition accuracy and >95% person detection precision.
Where Will Computer Vision Deliver the Greatest Impact?
While CV has applications across the entire manufacturing lifecycle, its benefits are not equally distributed. Some stages offer significantly higher returns than others. Manufacturers must prioritize where computer vision delivers the most value to allocate budgets and timelines wisely.
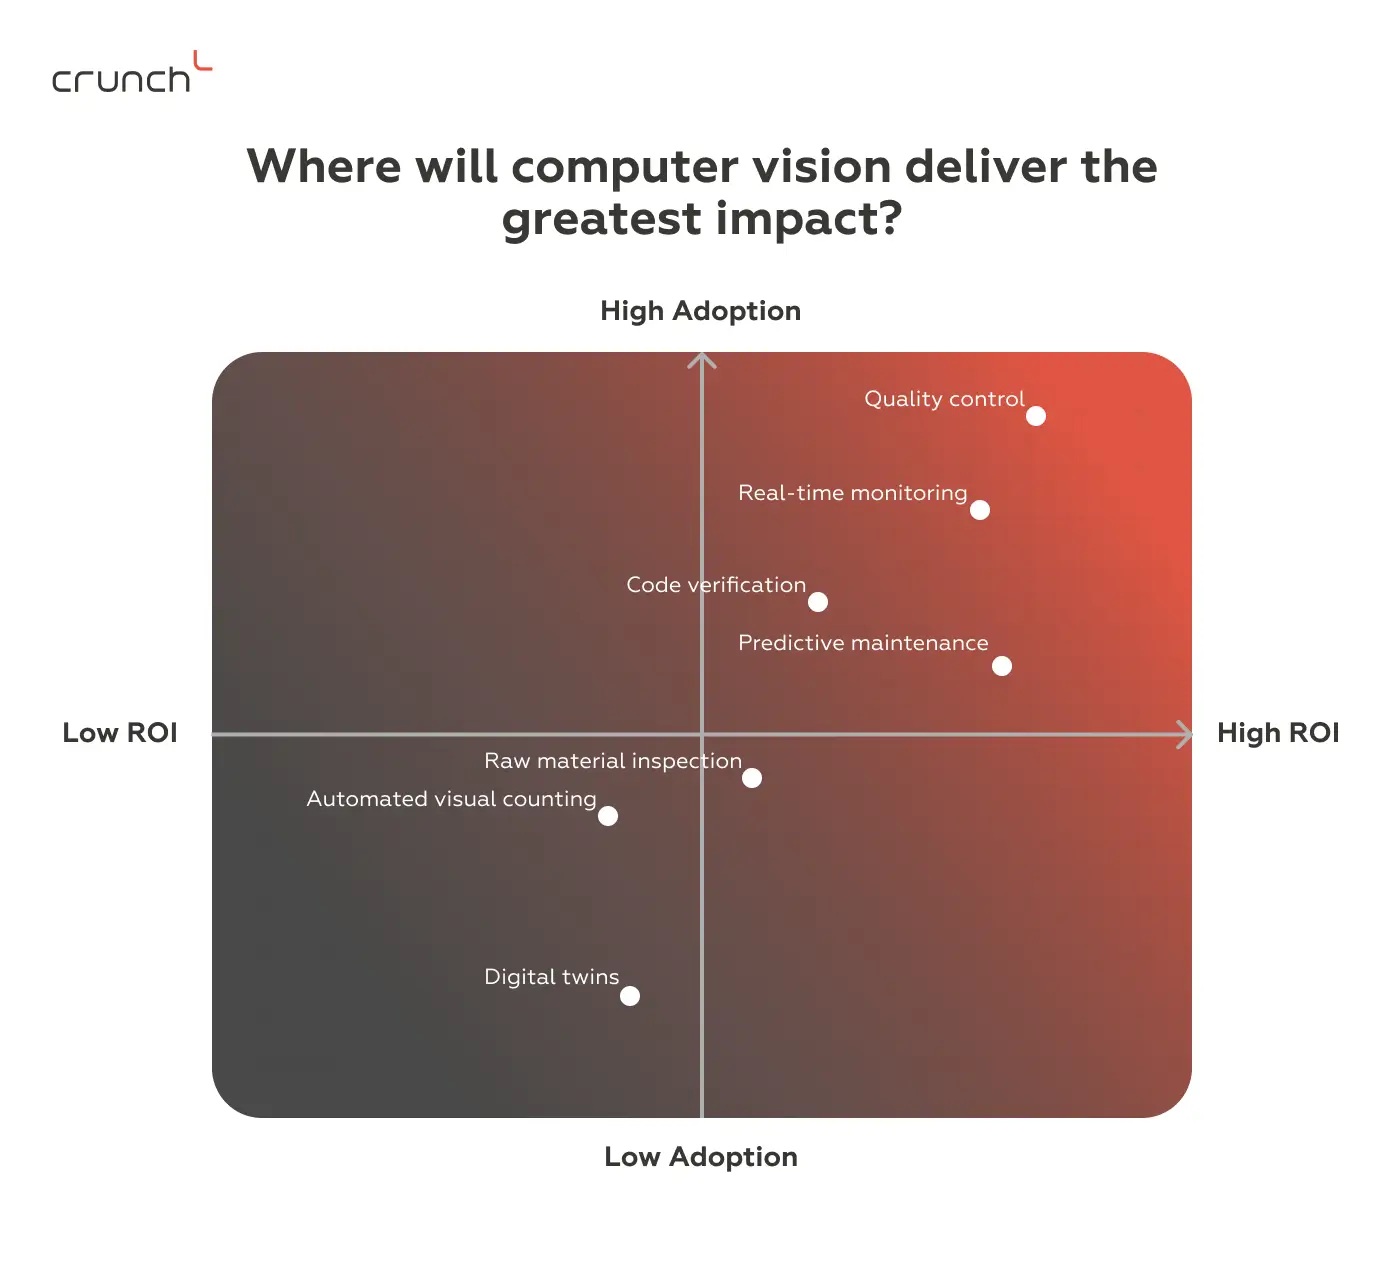
The illustration shows that quality control and inspection remain the most impactful areas. Similarly, in the production phase, real-time manufacturing process monitoring with computer vision helps catch process deviations or machine faults early, preventing defects and avoiding costly rework.
Another high-value application is predictive maintenance. By visually detecting signs of wear, misalignment, or overheating in equipment, manufacturers can avoid unplanned downtime, saving thousands per minute in lost productivity. Computer vision also enhances packaging and labeling, ensuring label placement, barcode readability, and seal integrity meet compliance standards, particularly in industries where traceability is essential.
While raw material inspection is often overlooked, detecting defects upfront ensures consistent inputs for manufacturing and reduces downstream waste. Other stages like distribution and logistics benefit from visual tracking of pallets and shipments, while product design is a growing area where computer vision supports faster iteration through digital twin validation and surface analysis.
To better understand the investments necessary to implement such solutions, please refer to our previous article: The 2025 Guide to Computer Vision Development: Costs, Process & Tech Stack
Computer Vision Challenges in Manufacturing
While computer vision offers immense benefits, implementation in manufacturing presents distinct challenges:
- The most cited problem is lighting inconsistency. Subtle variations in ambient light or inconsistent illumination severely impact image quality and algorithm accuracy. Achieving optimal lighting often requires specialized photometric expertise and, ideally, a controlled “black box” environment. Avoid external light sources like skylights.
- Minor differences in incoming colors, textures, or shapes can confuse computer vision.
- There’s a tendency to want the CV to do everything. Clearly defining the exact inspection task upfront is crucial.
- For lower-volume production, the initial investment in computer vision hardware and integration can be hard to justify against the benefits, making it most viable in high-volume environments where its speed and consistency offer a clear ROI.
Overcoming these challenges demands a blend of technical expertise, meticulous planning, and practical adaptation of both software and physical setup.
How to Implement Computer Vision in Your Manufacturing Process
Implementing computer vision in manufacturing industry environments requires a structured approach. Below is a practical step-by-step roadmap that reduces risk, controls cost, and ensures the solution delivers measurable value.
Step 1: Identify the Highest-Value Use Cases
Start by mapping your production workflow and identifying areas where computer vision use cases in manufacturing offer the greatest ROI.
Examples:
- computer vision quality control manufacturing (defect detection)
- computer vision in production monitoring (detecting machine deviations)
- computer vision for manufacturing safety (PPE, zone entry detection)
Focus first on processes that are:
- high-volume
- error-prone
- costly when defects occur
- dependent on manual inspection
Step 2: Conduct a Feasibility Assessment
Before jumping into development, evaluate technical readiness:
- Do you have historical image/video data?
- Are the lighting and camera positions stable?
- Is real-time processing required?
- Can your MES/SCADA integrate with CV outputs?
This helps determine whether you need on-prem servers, edge devices, or cloud-based computer vision manufacturing solutions.
Step 3: Run a Discovery Phase
A Discovery Phase helps define the entire project before building. It typically includes:
- Clear business problem definition
- Documented high-level requirements & workflows
- AI-ready planning documentation for faster implementation
This de-risks the project and ensures alignment with business goals.
Step 4: Build a Proof of Concept (PoC)
A PoC tests whether the model can reliably detect defects or patterns in a controlled environment.
A solid PoC includes:
- training initial computer vision AI in manufacturing models
- testing multiple architectures to find the best fit
- validating performance against real defects
- running edge inference tests if needed
The goal is not to automate instantly, but to prove the model works.
Step 5: Deploy a Pilot on One Production Line
Once the PoC succeeds, the next step is piloting. You evaluate real-world accuracy, false positive rate, and operational stability.
Step 6: Iterate and Scale Across Lines or Plants
After the pilot delivers results:
- fine-tune the model on new data
- retrain when materials or suppliers change
- standardize camera and lighting setups
- create a scalable architecture for other lines
A mature deployment includes dashboards for:
- defect trends
- downtime analytics
- throughput metrics
This transforms CV into a long-term computer vision solution for manufacturing.
Step 7: Enable Continuous Improvement
To maintain accuracy, companies must:
- monitor model drift
- retrain with new defect types
- recalibrate cameras periodically
- update AI models as product designs evolve

How can Crunch-IS Help You with Computer Vision for the Manufacturing Industry?
Crunch-IS is a full-service technology provider, and partnering with us equals cost reduction + greater scalability + better efficiency + fast delivery.
For manufacturing companies looking to leverage computer vision, Crunch-IS offers comprehensive support tailored to your specific needs:
- If you have a raw idea for how computer vision could transform your manufacturing process, we’ll start with a discovery phase. During this crucial stage, our experts will collaborate with your team to understand your challenges, explore potential applications, and propose concrete solutions that align with your business objectives.
- If you already have a clear vision and defined requirements for your computer vision project, we are prepared to commence the project immediately. Our experienced teams can seamlessly integrate into your workflow, leveraging their in-depth technical capabilities to develop and implement robust computer vision solutions for manufacturing that deliver tangible results in a timely manner.
Whether your objective is to enhance quality control, boost efficiency, improve safety, or gain deeper insights into your operations, Crunch-IS provides the expertise and resources to help you achieve your goals.
Our experts are always pleased to provide a free consultation. So, if you have an idea (or would like to discuss how we can help), you can contact us at your convenience.